Capabilities
Ten processes under one roof
One factory, six major manufacturing processes — forging, die casting, stamping & welding, rubber vulcanization, machining and assembly — backed by four supporting operations from heat treatment to X-ray detection. It is why we can hold tolerance, traceability and lead time on 9,500+ part numbers in catalogue, including 1,800+ aluminum control arm references.
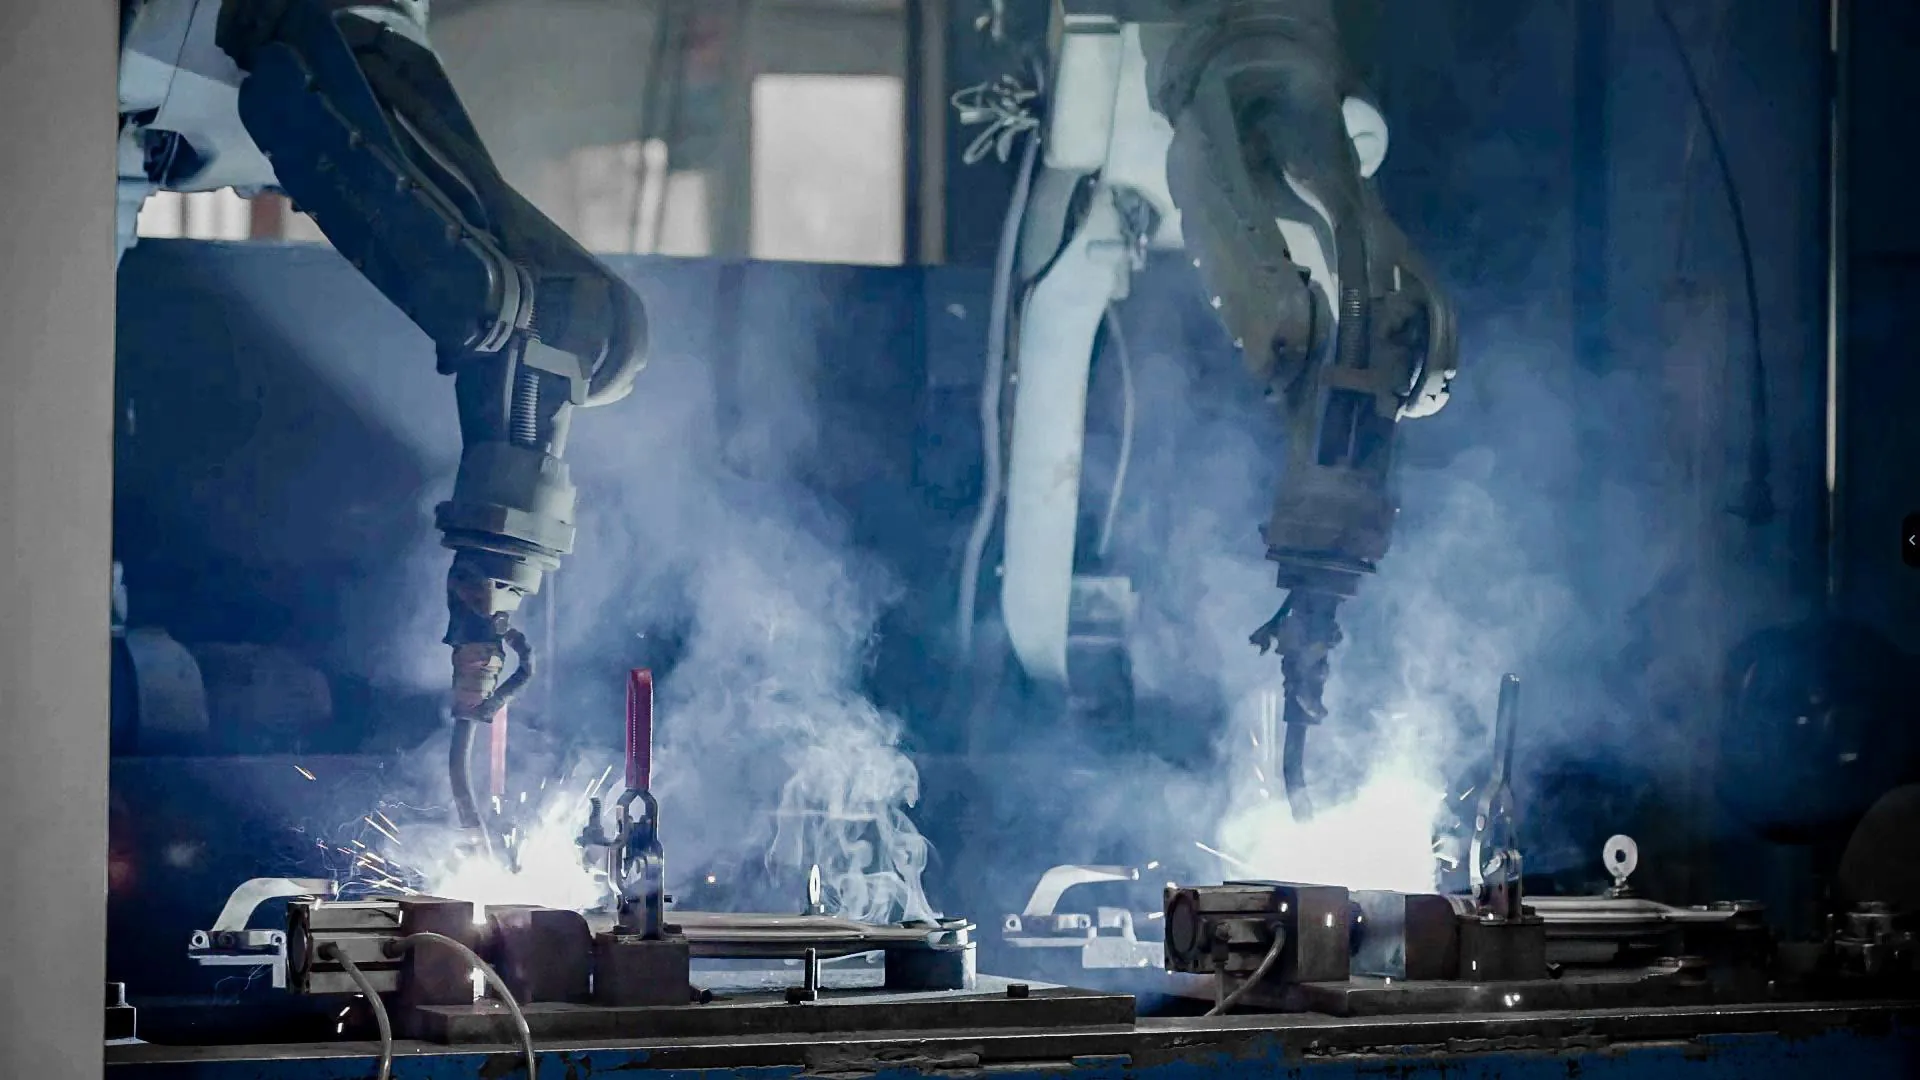
Robotic welding cell, Wuhu plant · part of the 9,500 m² stamping & welding shop.
Plant at a Glance
160,000 m² of in-house capacity
10
Aluminum forging lines, largest press 6,300 T (plus 2 steel lines)
12
Die casting machines from 160 T to 800 T — 9 high-pressure + 3 low-pressure
10
Welding robots and 25+ presses (60 T–315 T) in the stamping & welding shop
30+
Rubber injection vulcanizing machines, plus 8 hydraulic presses
108
Machining centers — 88 vertical + 20 horizontal
Six Major Processes
Forging, casting, stamping, rubber, machining & assembly
The six major processes that shape a chassis part — all inside our own walls, from billet and ingot to the finished, boxed assembly.
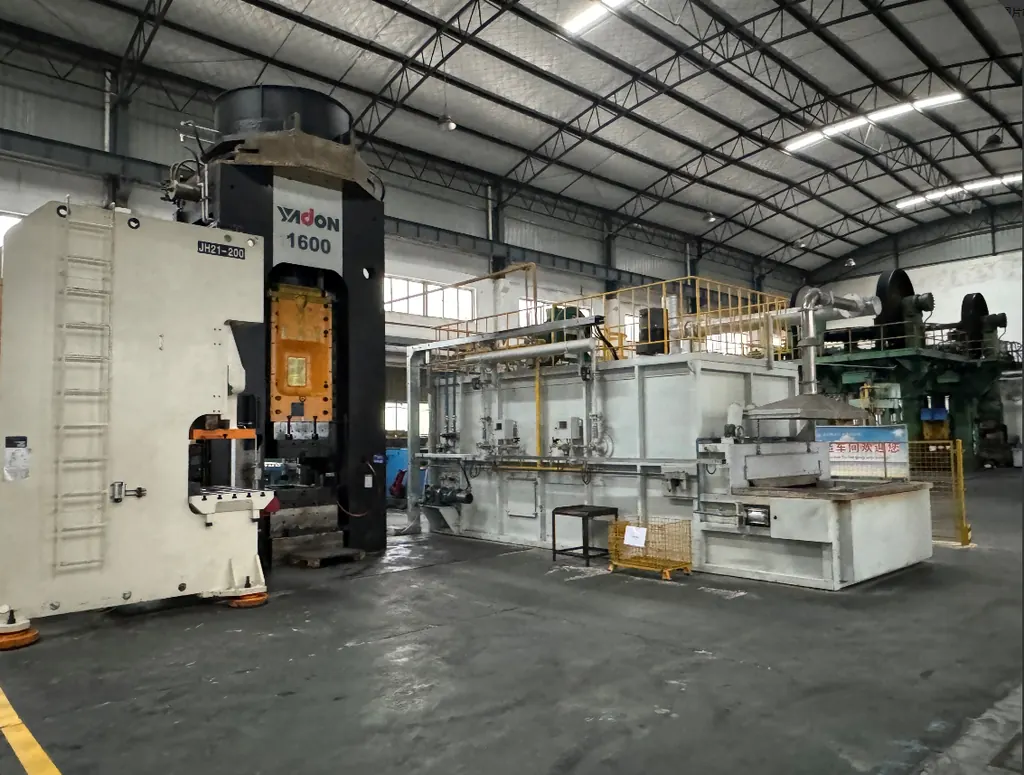
12,000 m² · 7M pcs/yr
Forging
10 aluminum forging lines — 2×6,300 T, 2×2,500 T, 4×1,600 T, 2×1,000 T — plus 2 steel forging lines (2×2,500 T). Control arm bodies, steering knuckles, ball joint housings.
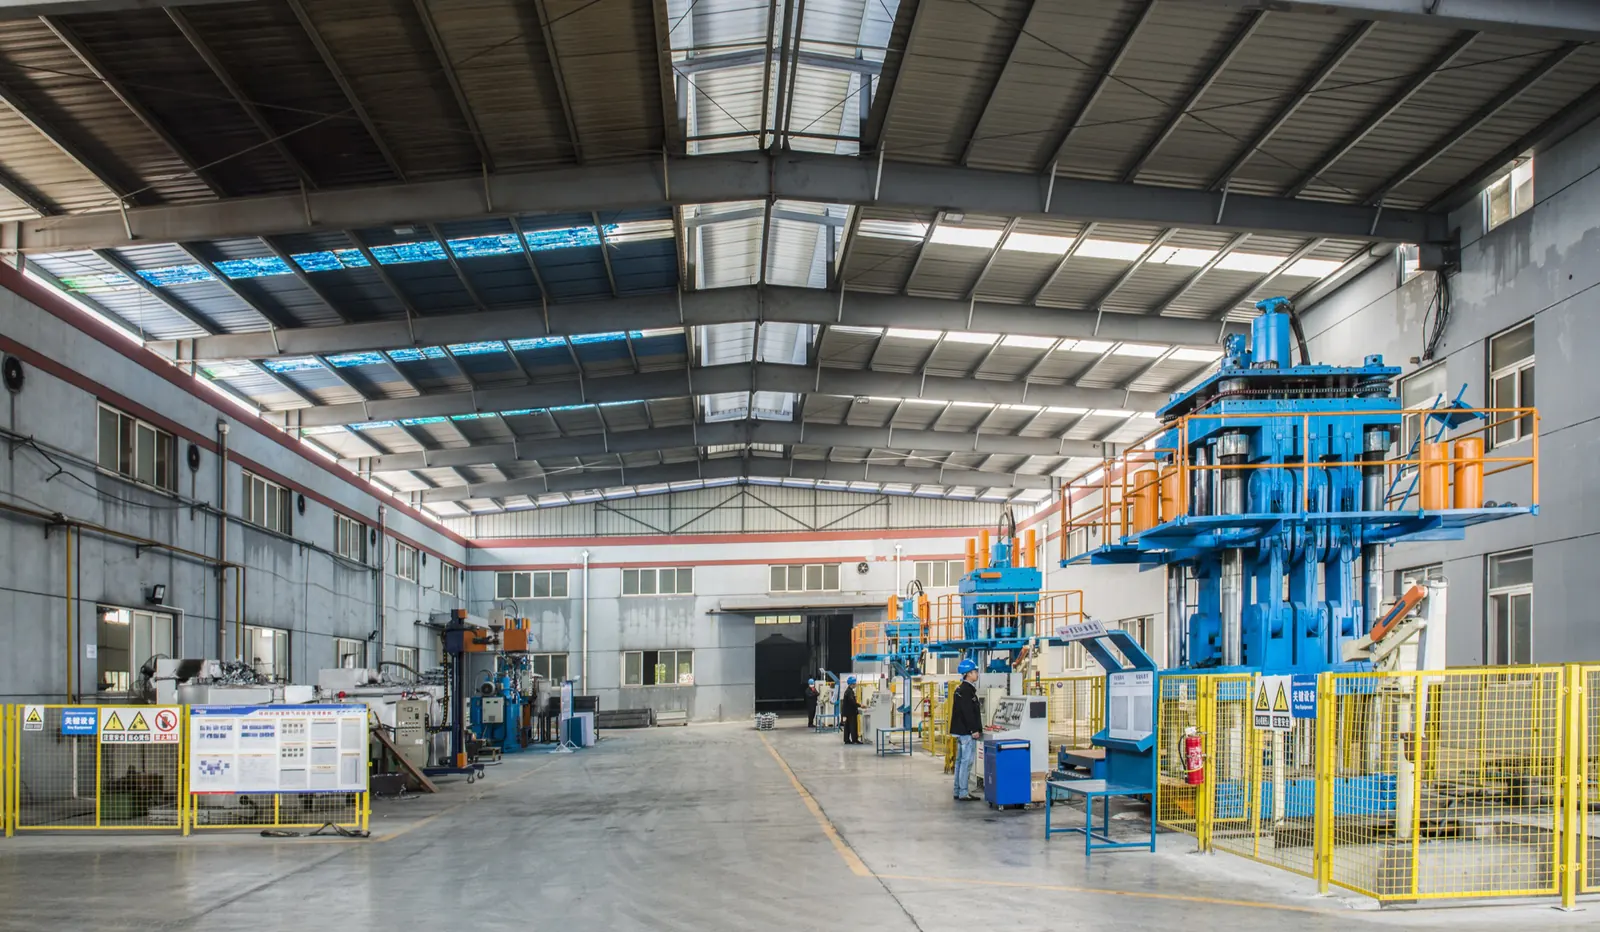
6,002 m² · 2M pcs/yr
Die Casting
9 high-pressure machines — 2×160 T, 3×280 T, 1×400 T, 2×500 T, 1×800 T — plus 3 low-pressure machines. Die-cast control arms, engine and transmission mount housings.
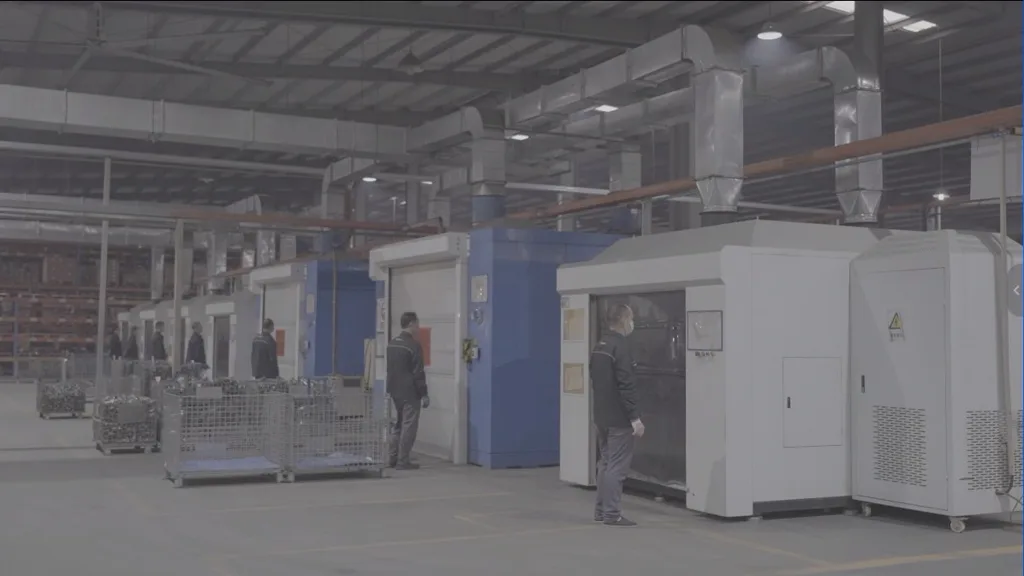
9,500 m² · 1.2M pcs/yr
Stamping & Welding
25+ presses from 60 T to 315 T and 10 welding robots. Brackets, mounting plates and welded assemblies for stamped control arms and stabilizer links.
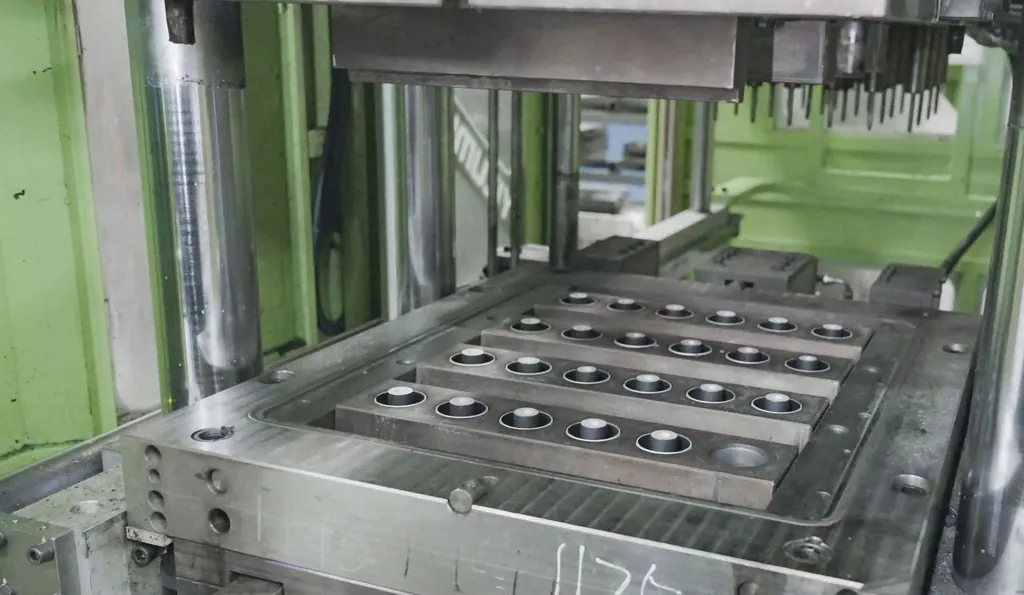
18,365 m² · 10M pcs/yr
Rubber Vulcanization
30+ vulcanizing injection machines, 8 hydraulic presses and dedicated hydraulic mount & bushing filling lines — in-house compound mixing for bushings, mounts and strut mounts.
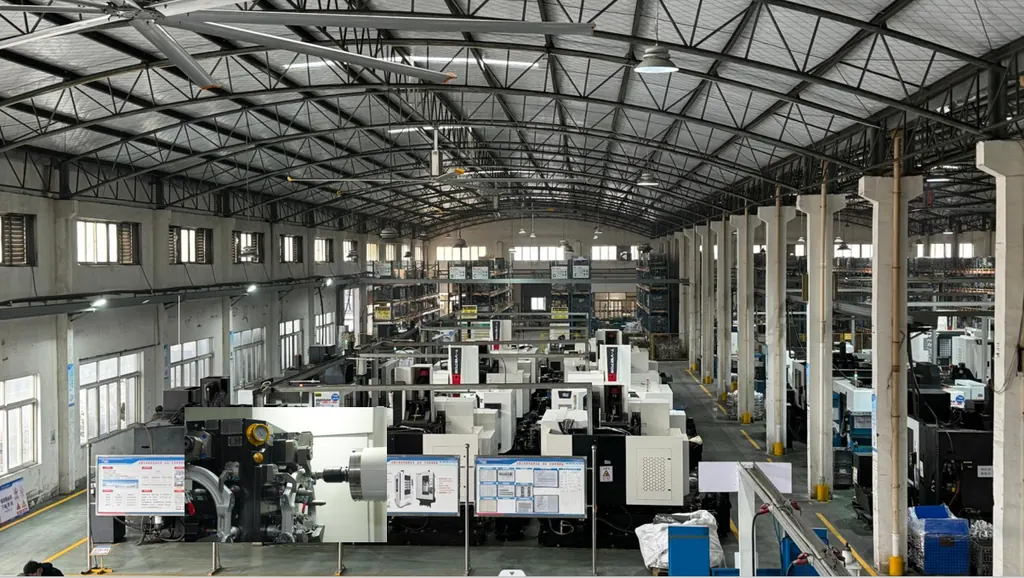
4,000 m² · 6M pcs/yr
Machining
88 vertical + 20 horizontal machining centers — bushing bores, ball joint seats and mounting faces, plus in-house molds, jigs and gauges.
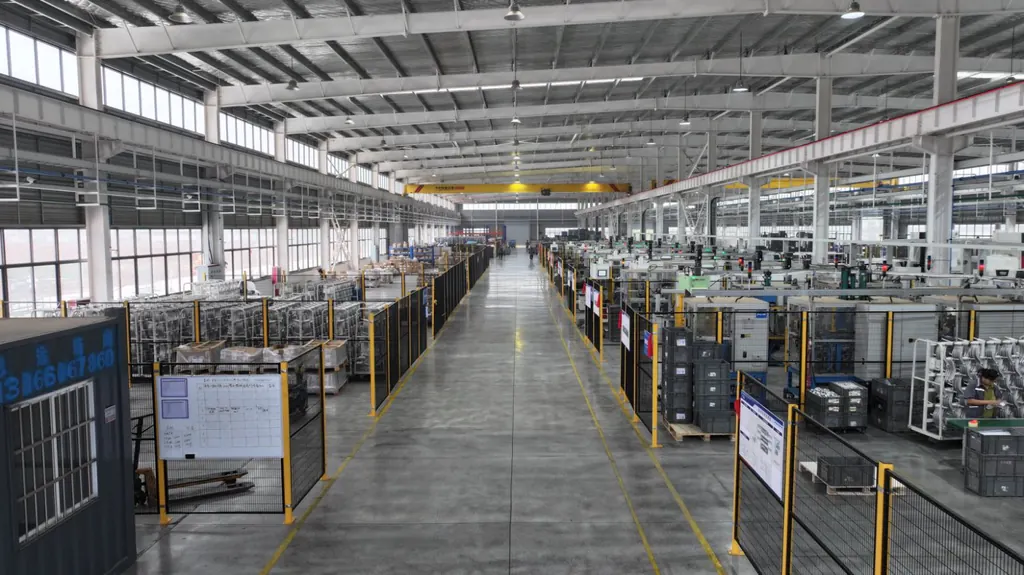
4,000 m² · 6M pcs/yr
Assembly
Dust-cover pre-assembly, spin riveting, lubricant injection, air-tightness testing, torque & swing-angle measurement and QR-code laser marking.
Supporting Operations
Four operations that finish the part
Heat treatment through final X-ray detection — the steps between a raw shape and a boxed, traceable part.
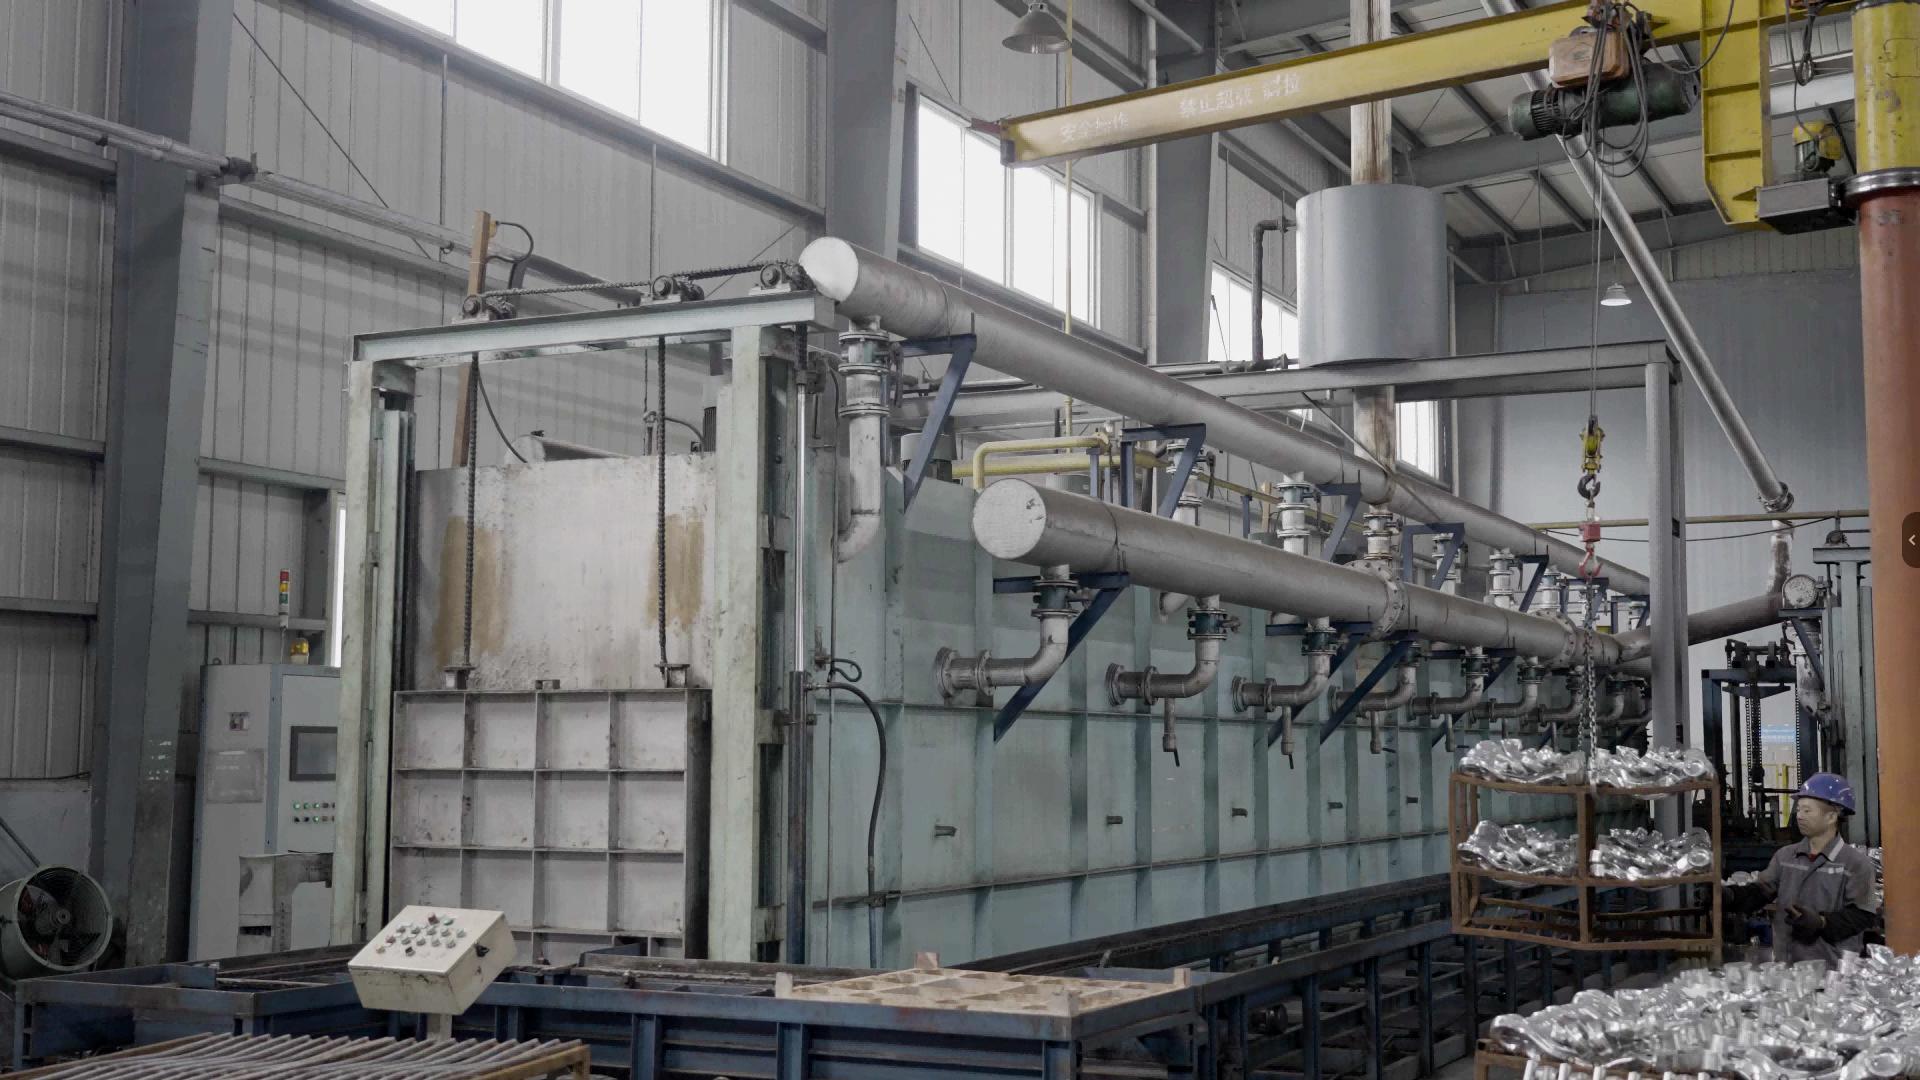
2,000 m² · 6M pcs/yr
Heat Treatment
Solution and aging furnaces for aluminum forgings — hardness and grain structure controlled batch by batch.
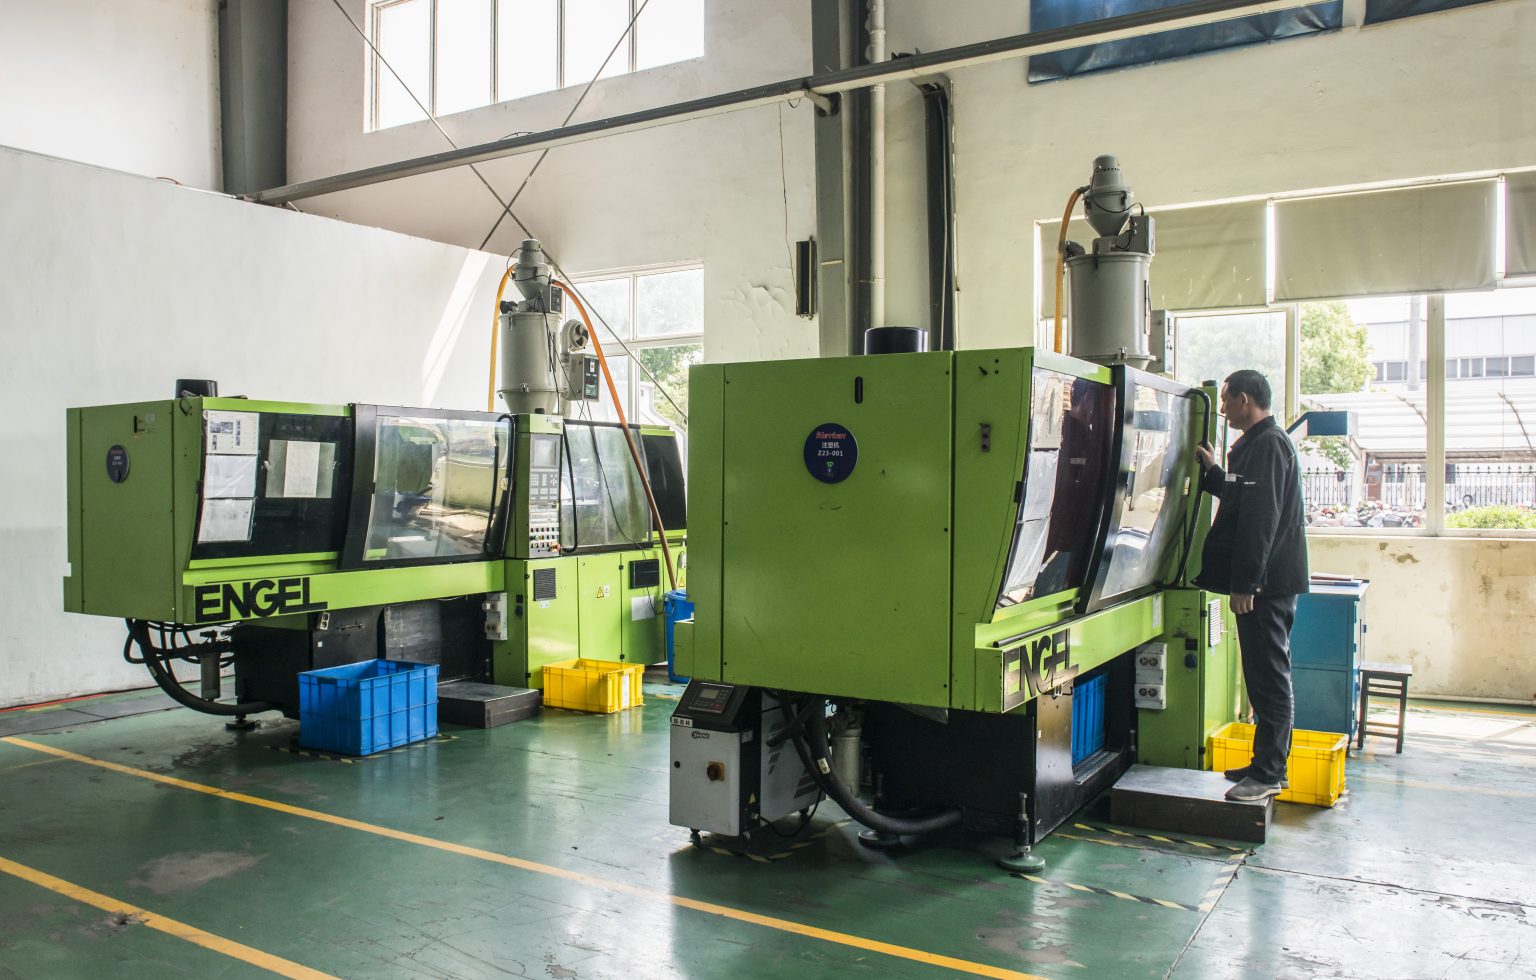
1,850 m² · 6M pcs/yr
Injection Molding
2×270 T + 2×330 T injection machines for technical plastic components of mounts and strut mounts.
2,000 m²
Fluorescence Inspection
3 automatic fluorescent penetrant inspection lines — surface crack detection on 100% of safety-critical forgings.
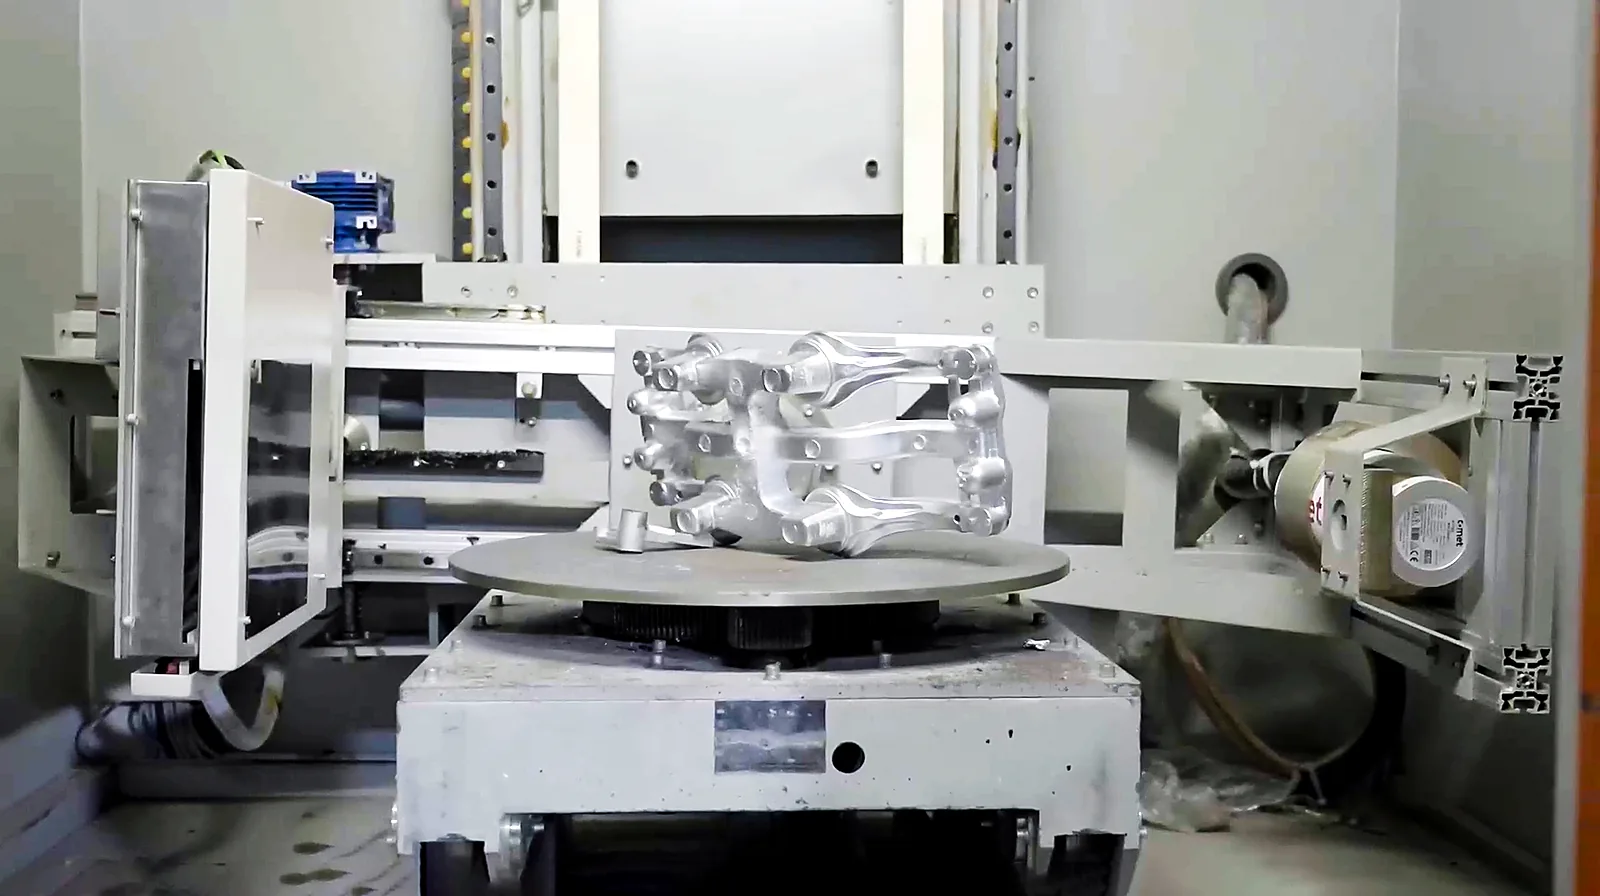
8,800 m² · 1M pcs/yr
X-ray Detection
X-ray cabinets checking die castings for internal porosity — the same chamber inspects forged arms before machining.
Inspection & Traceability
Every batch verified, every part traceable
Process control does not stop at the end of the line: penetrant and X-ray inspection sit inside the plant, and material verification runs in our CNAS-accredited laboratory — spectral analysis, metallography and fatigue benches for every material batch.
Downstream quality follows the same chain: 50+ specialists across 11 quality functions, first response to every complaint within 24 hours. Read more on quality & certification, or how our engineers develop a part from concept to SOP.
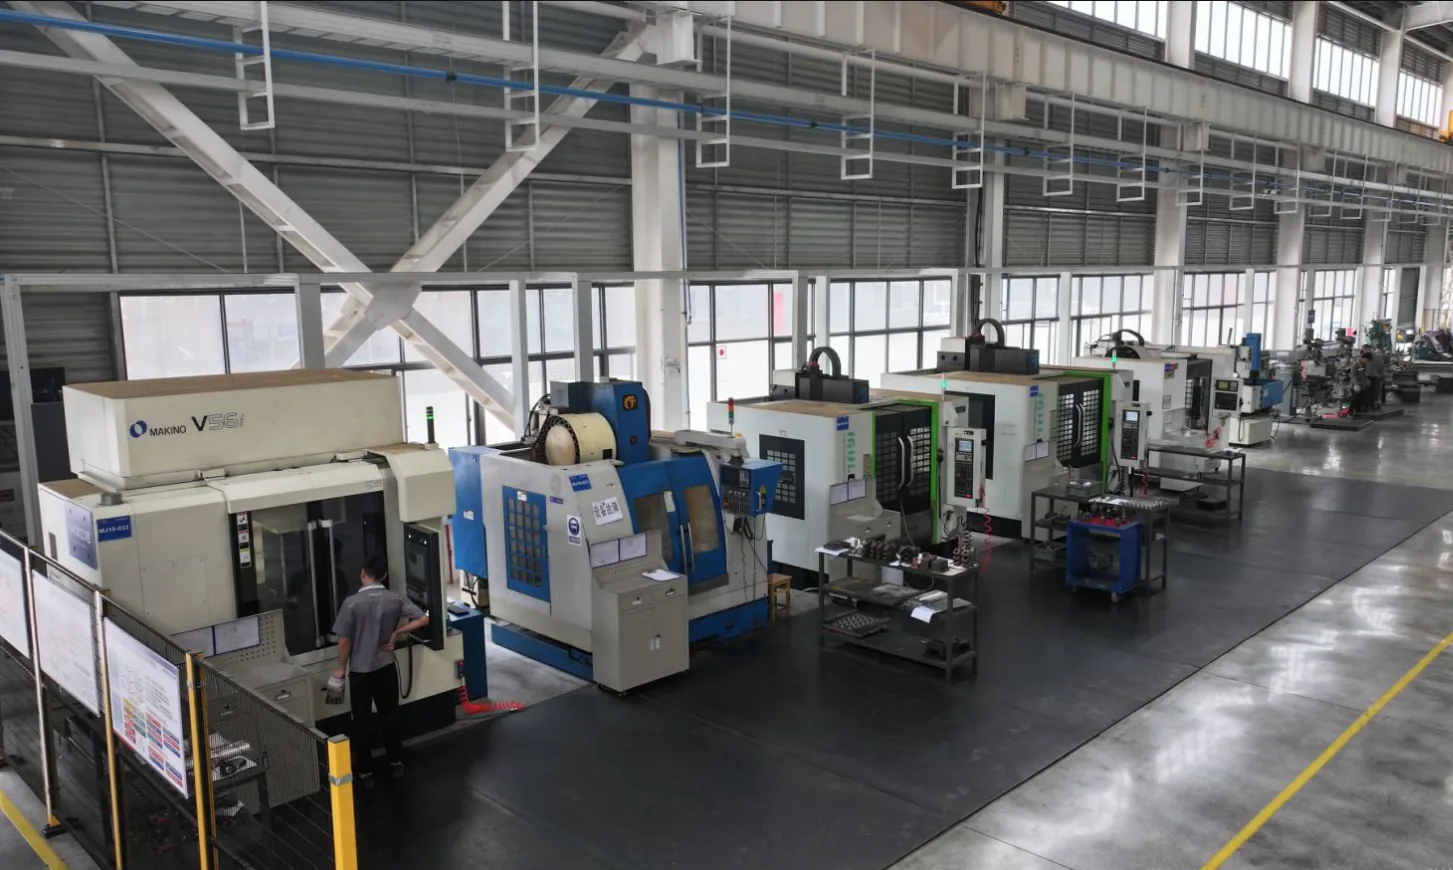
Tooling
The in-house mold workshop behind every process
A dedicated 3,200 m² workshop with 32 specialists designs and manufactures the molds for all six major processes — seven mold families, from rubber vulcanization to cold extrusion, built in-house instead of bought.
Next Step
Audit our plant, or start with a part number.
Technical question about a process? Our after-sales team gives first feedback within 24 hours.